0
About Gemmymedical
About Gemmymedical
Since 2009 - All for Better Health
Gemmytec is a National High-Tech Enterprise and a Shanghai Specialized and Sophisticated SME, specializing in intelligent disinfection systems, medical consumables, and digital hygiene management solutions. Guided by our mission “All for Better Health”, we build an integrated hygiene management system covering healthcare, food safety, and public hygiene, delivering safe, efficient, and intelligent solutions for global customers. Gemmytec originates from GemmyMedical, which focused on medical disinfection, infection control, and personal protection solutions. Built on its early expertise in healthcare hygiene and infection prevention, the company has continuously evolved through industrial upgrading and strategic expansion, establishing Gemmytec (Shanghai) Co., Ltd. in Shanghai as its global operations center, innovation hub, and manufacturing coordination base. Driven by continuous innovation and global resource integration, Gemmytec is committed to transforming hygiene management from a single healthcare focus into an integrated ecosystem spanning healthcare, food service, and public environments.
17+
Production Experience
100+
Global Partners
100+
Intellectual Properties
10000+
Factory Area

Who We Are

With over 17 years of development, Gemmytec has evolved from a specialized healthcare hygiene company into a comprehensive health technology enterprise integrating R&D innovation, smart manufacturing, digital systems, and global trade. With headquarters in Shanghai, an international trading hub in Hong Kong, and strategic manufacturing partners in China, we operate a globally coordinated ecosystem covering innovation, production, and supply chain management. We are committed to building a unified hygiene management system across three key sectors:

  • Healthcare infection control and clinical safety
  • Food processing and front- & back-of-house hygiene management
  • Public and commercial environmental hygiene protection

What We Do

Gemmytec builds its business around a clear development pathway: Disinfection → Protection → Care → Health Management, and operates through three core business pillars:

Intelligent Disinfection Systems
We provide disinfection products, equipment, and intelligent solutions for healthcare, food-service, and public environments. Our proprietary Atomic Water Disinfection Technology is based on advanced electrochemical principles, delivering a chemical-free, low-energy, and environmentally friendly disinfection solution widely used in hospitals, commercial kitchens, and public spaces. Our intelligent disinfection robots integrate AI and IoT technologies to enable automated space disinfection, hand hygiene services, and digital hygiene management across hospitals, food-service facilities, and public areas.

Medical Consumables & Care Products
We offer a comprehensive portfolio of medical consumables, including wound care products, ostomy care solutions, and personal protective equipment (PPE). Our products are widely used in hospitals, clinics, long-term care facilities, and home healthcare environments, and also extend into the food-service industry for basic hygiene and personnel protection needs.

Digital Hygiene Management Systems
Through IoT, AI, and big data technologies, Gemmytec has developed a Hand Hygiene Monitoring and Management System, extended to both healthcare and food-service environments.
Global Presence
With headquarters in Shanghai and an international trading hub in Hong Kong, Gemmytec has built a global operational network integrating R&D, manufacturing, supply chain management, and international trade.
Our solutions are widely used in healthcare institutions, food-service chains, and public environments across Asia, Europe, the Middle East, Africa, and the Americas, forming a continuously expanding global footprint.
Our Vision
Looking ahead, Gemmytec will continue to drive innovation in intelligent health management, advancing the digital transformation of healthcare, food safety, and public hygiene systems.
We believe health is not only a need, but a system capability.
Guided by “All for Better Health,” we are committed to building a safer, greener, and more intelligent global health ecosystem.
Our Core Values

All for Better Health: At Gemmytec, our mission goes beyond products and technologies. We are committed to creating safer, healthier, and more sustainable environments through innovation, responsibility, and continuous improvement.
Innovation: We continuously invest in technology, research, and product development to create smarter solutions for disinfection, healthcare, food safety, and hygiene management.
Quality: Quality is at the center of everything we do. From product design and manufacturing to service delivery, we maintain rigorous standards to ensure reliability, safety, and performance.
Responsibility: We take responsibility for protecting human health, supporting our customers, and contributing to safer communities through effective hygiene and infection prevention solutions.
Sustainability: We believe innovation should benefit both people and the planet. Through green technologies, sustainable manufacturing, and resource-efficient solutions, we work toward a healthier future for generations to come.
Collaboration: We build long-term partnerships with customers, distributors, healthcare professionals, and industry partners to create greater value and achieve shared success.
Customer Focus: Understanding our customers' needs is the foundation of our business. We strive to deliver practical, efficient, and tailored solutions that help our customers improve hygiene, safety, and operational performance.
Production experience Production experience
17
Production experience
Intelligent Production Lines Intelligent Production Lines
15
Intelligent Production Lines
Global partners Global partners
100
Global partners
Ship to country Ship to country
30
Ship to country
Has 3 subsidiaries Has 3 subsidiaries
5
Subsidiaries
Products enter pharmacies Products enter pharmacies
100
Products enter hospitals
Factory area (m2) Factory area (m2)
100000
Factory area (m2)
Obtain special certificate Obtain special certificate
100
Obtain special certificate
PROTECT THE HEALTH OF EVERY USER
All for Better Health
Looking ahead, Gemmytec will continue to drive innovation in intelligent health management, advancing the digital transformation of healthcare, food safety, and public hygiene systems. We believe health is not only a need, but a system capability. Guided by “All for Better Health”, we are committed to building a safer, greener, and more intelligent global health ecosystem.
OUR
HISTORY

Since its establishment, Gemmytec has continuously expanded its presence in intelligent disinfection and health management, building a global business ecosystem.

OUR FACTORY
FROM CUSTOM DEVELOPMENT TO MASS PRODUCTION

With modern manufacturing facilities and experienced engineering teams, GemmyMedical provides flexible OEM, ODM, and private-label solutions while maintaining the highest standards of quality, safety, and regulatory compliance.
100,000,000+
Yearly Capacity (PCS)
100,000+
Factory Area (m2)
500+
Number of Employees
15+
Automated Production Lines
MANUFACTURING FACILITY

We operate multiple production bases strategically located across Shanghai, Guangdong, Zhejiang, and Henan, China. Spanning over 100,000 m² combined and staffed by approximately 500 skilled personnel, our facilities are the engine behind our medical supply production—delivering infection control, ostomy care, wound care, PPE, and cosmetics solutions to healthcare professionals and home care users worldwide. Every product line is managed by dedicated cross-functional teams covering R&D, quality assurance, production, and logistics. Through continuous R&D investment, proprietary production technologies, and a customer-first development philosophy, we ensure every decision—from raw material sourcing to final inspection—is built around meeting and exceeding international medical device standards.

PRODUCTION VIDEO
FACTORY VIDEO
Know more details of our factory in the video.
LAB
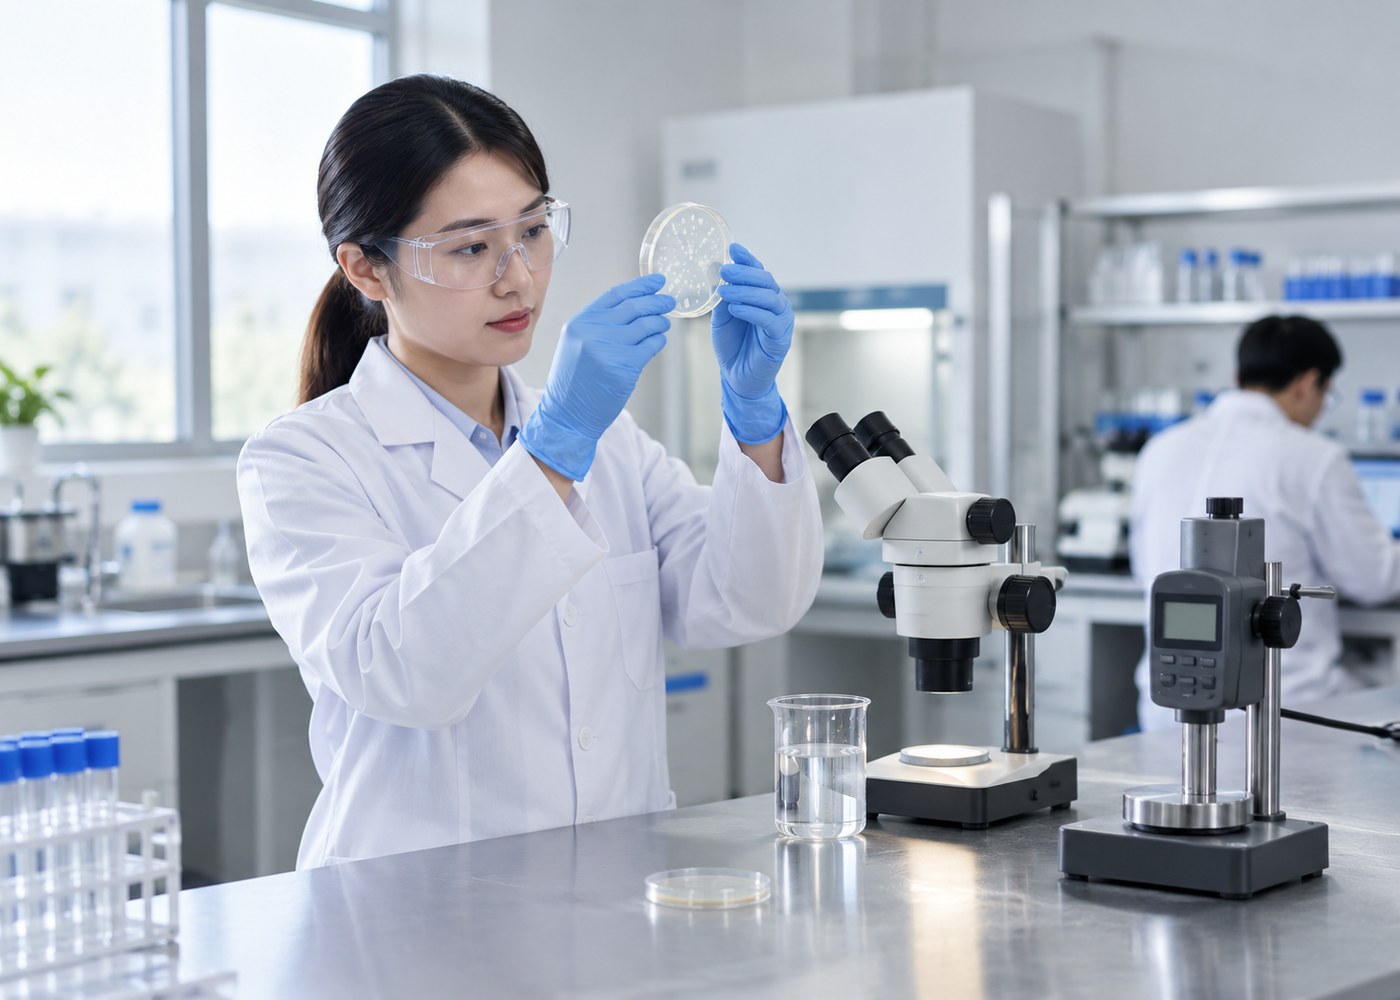
Quality control laboratory at GemmyMedical testing infection control and medical consumable products
QUALITY LAB
Our Quality Lab is where our commitment to quality becomes measurable. It is the in-house testing centre for the whole GemmyMedical range: hand sanitizers, disinfectant wipes, surface disinfectants, wound dressings and ostomy care products. Formulation work, raw material verification, in-process sampling and finished-goods release testing all happen under one roof, following an ISO quality management system for market access. Every batch is checked against agreed specifications, from active-ingredient concentration and pH to microbial limits, seal integrity and appearance. That is how we make sure a product performs the same way in a hospital in Doha as it does in the batch record from Shanghai. Trust in GemmyMedical means trust in quality you can verify.
EVERY BATCH TESTED IN OUR OWN LAB BEFORE IT SHIPS
CONTACT US
TESTING OF MEDICAL SUPPLIES
An overview of the tests our products undergo, the equipment we use, the methods we apply and the standards we test against, covering both our infection control lines and our wound and ostomy care ranges. The aim is simple: what we ship has to be safe, reliable and effective in the hands of the people who use it.
RAW MATERIAL TESTING
At GemmyMedical we test more than the finished product. The materials that go into our disinfectants, wipes and dressings are verified in our own lab before a production run starts, because the quality of the input sets the ceiling on the performance of the output. These are the incoming-material checks our QC team runs most often.
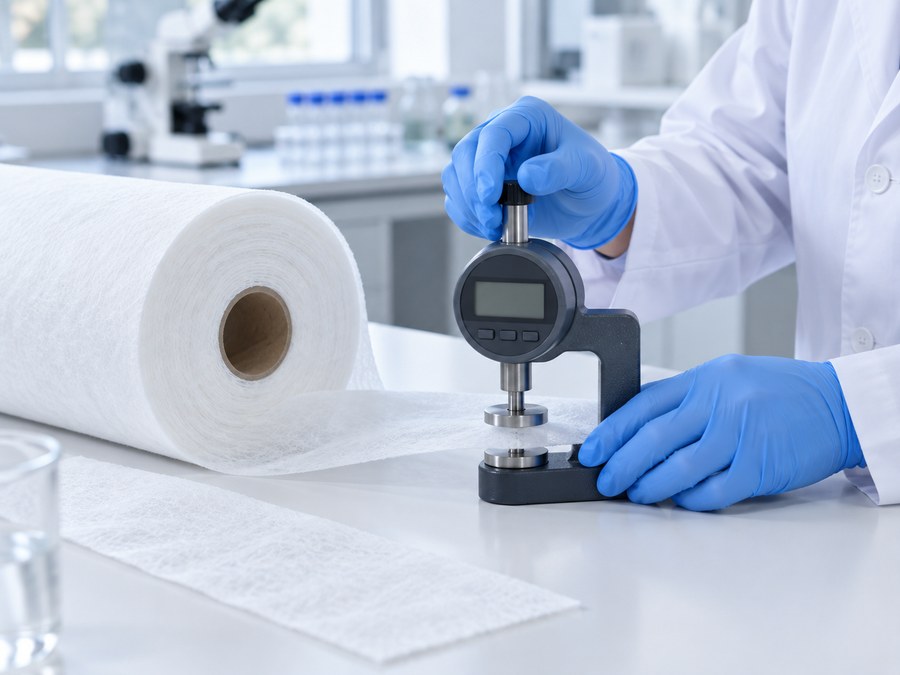
Spunlace nonwoven fabric inspection for medical wet wipes
SPUNLACE NONWOVEN TESTING
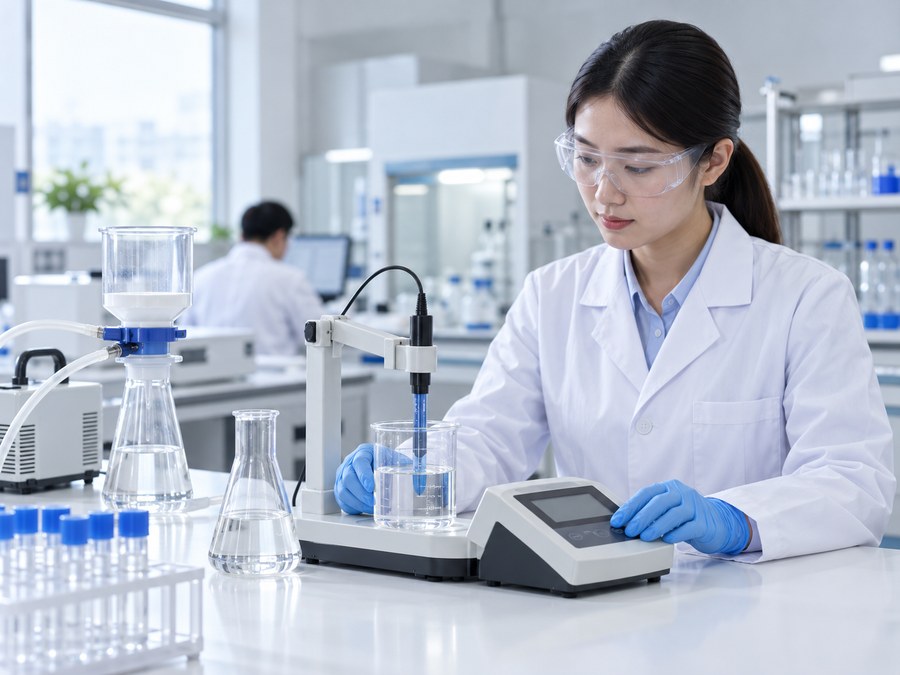
Purified water and liquid formula testing in the GemmyMedical lab
PURIFIED WATER & LIQUID FORMULA TESTING
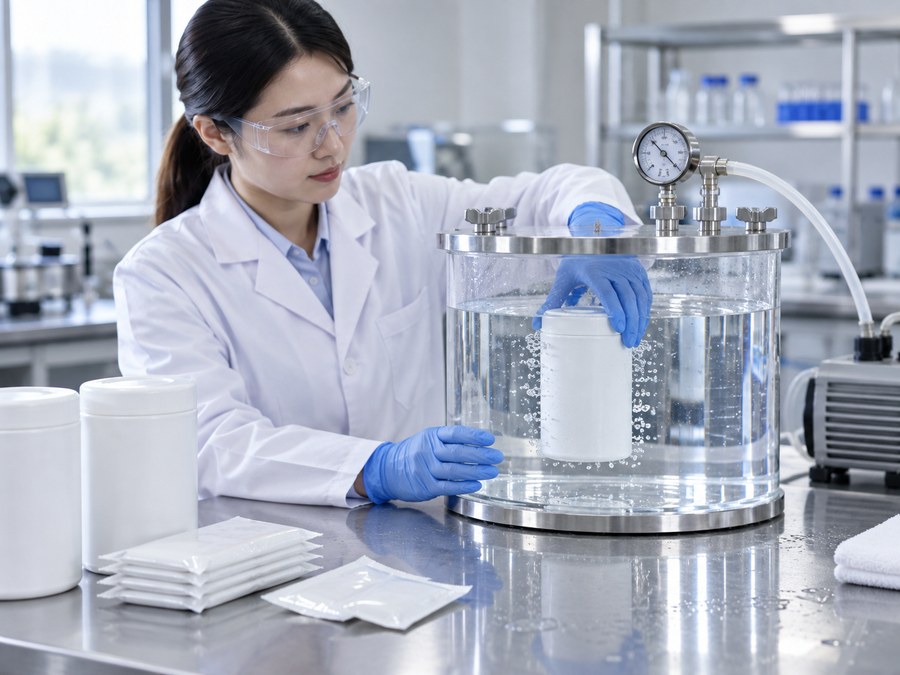
Packaging seal integrity testing for wet wipe canisters and sachets
PACKAGING SEAL INTEGRITY TESTING
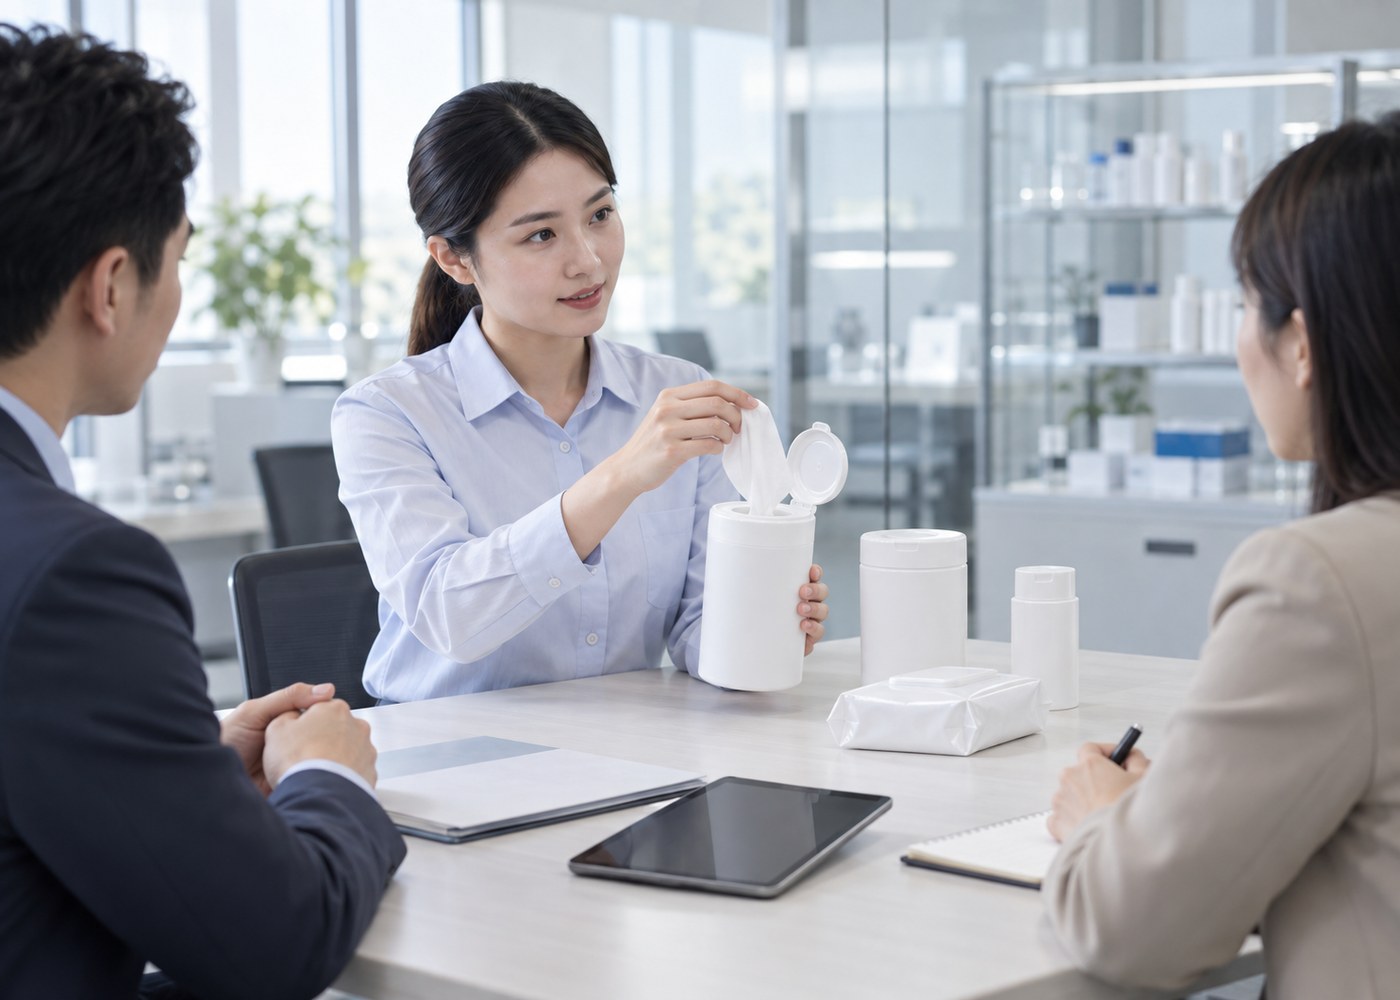
GemmyMedical product specialist helping a distributor choose infection control products
WHAT PRODUCT IS BEST FOR YOU
Distributors and procurement teams come to us with the same question: which product actually fits this market? Our specialist team works from the test data and the regulatory file of each SKU, so the recommendation you get is based on evidence rather than on a catalogue page.
Tell us your target market, sales channel and expected volume, and we will map it to the right product, packaging format and documentation set. For OEM and private-label buyers we can also adjust formulation, packaging and labelling to match your market requirements.
CONTACT US
SUSTAINABILITY

Sustainability at GemmyMedical is a manufacturing discipline rather than a slogan. Our guiding principle, All for Better Health, covers two things at once: the health of the people who use our products, and the environment of the factories that make them.

We concentrate on the three areas where a medical consumables manufacturer can make the biggest difference: cleaner production, lower-impact packaging and water stewardship. Our wet wipe lines run on an in-house EDI purified water process built from reverse osmosis, electrodeionisation, UV treatment and 0.22 micron final filtration. Our cleanrooms are managed to pharmaceutical-grade environment control. And the electrolysed water (BDD) technology developed within our group disinfects without added chemicals or consumables, which reduces both chemical discharge and the volume of packaging that has to be disposed of.

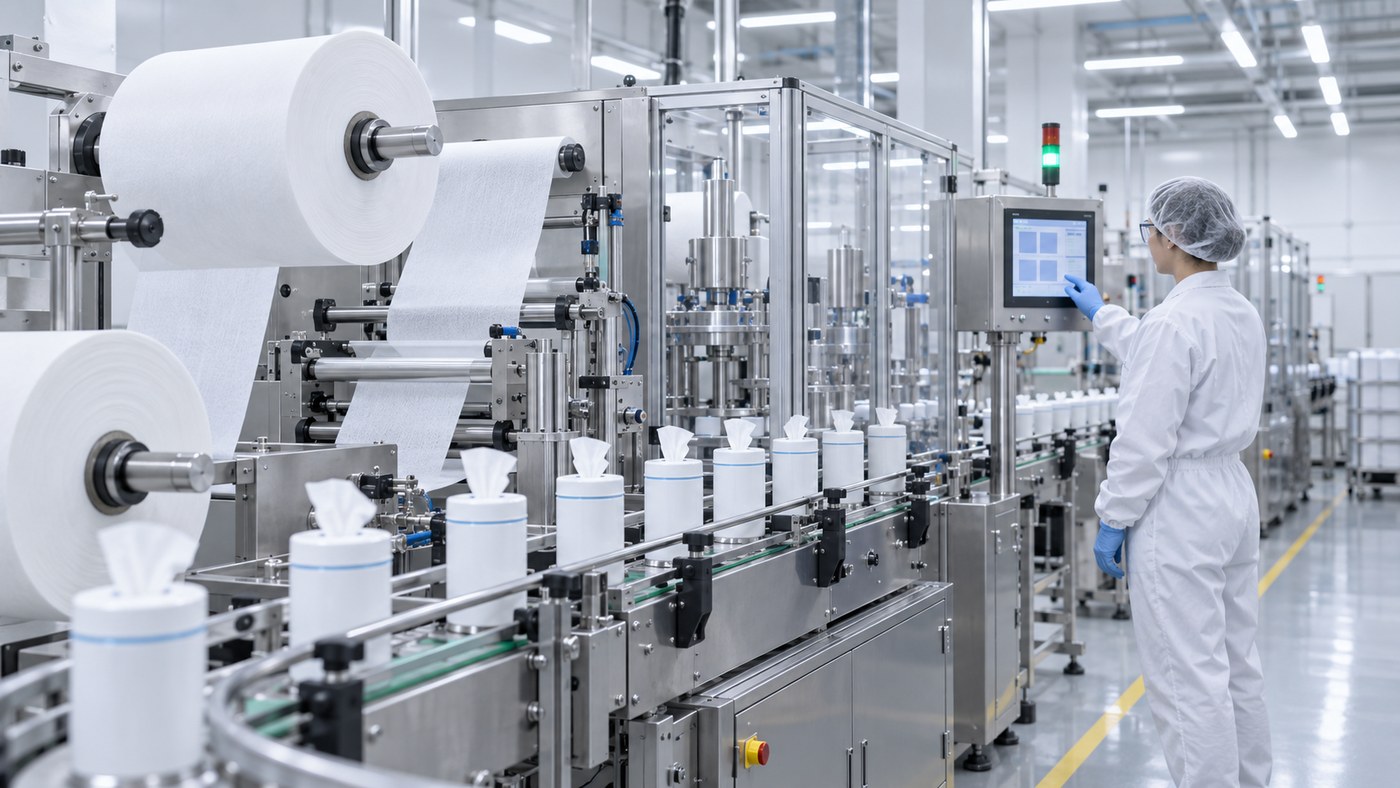
Digitally monitored automated wet wipe production line at GemmyMedical
Digitally monitored production lines
Our production equipment is monitored digitally from end to end. Automated wet wipe and liquid filling lines capture output, temperature, humidity and process parameters in real time, so a deviation is flagged while the batch is still running instead of being discovered afterwards. The same system keeps batch traceability records and feeds our Environmental and Safety (ES) controls, which watch the site continuously and are designed to trigger an immediate response to any incident.
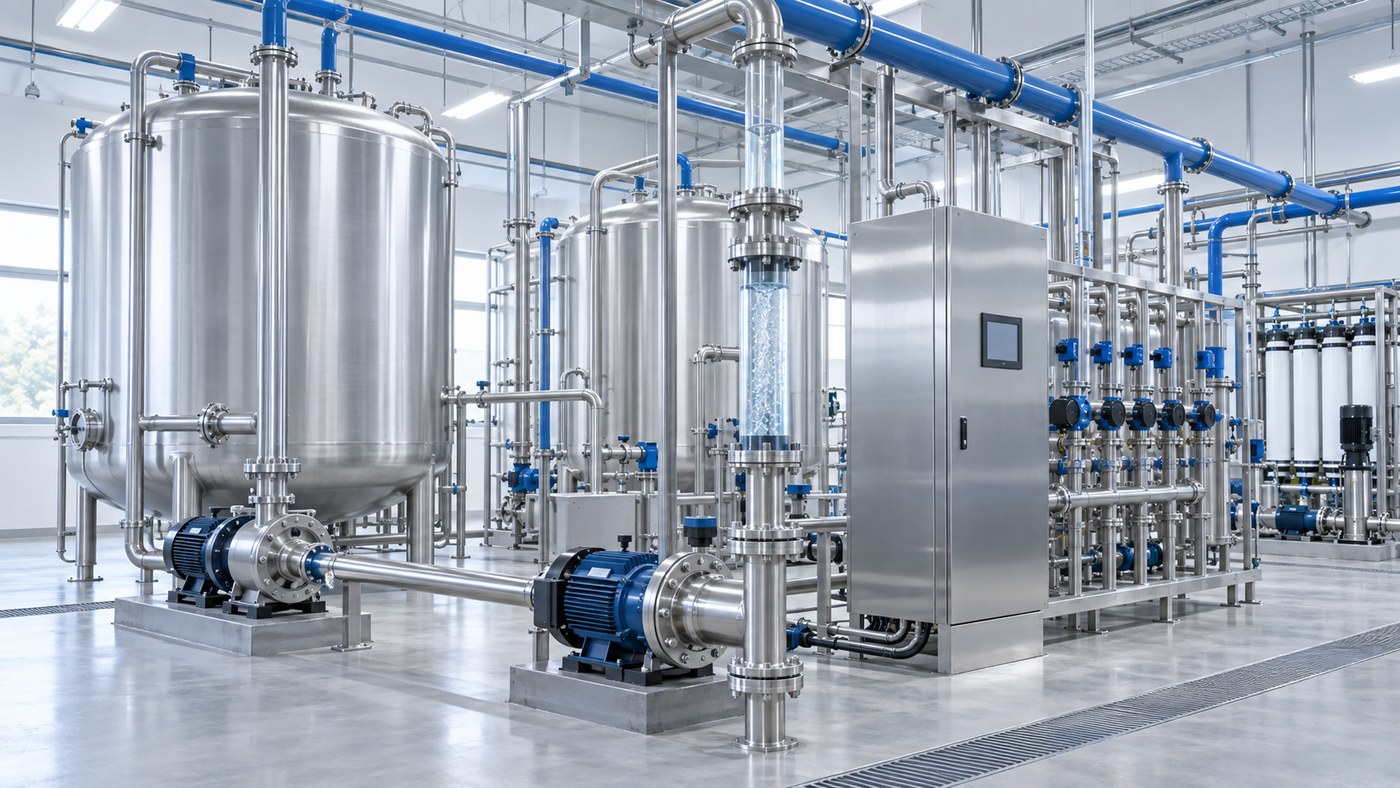
Water treatment and recycling system at the GemmyMedical manufacturing site
Waste treatment and recycling
Medical consumables manufacturing consumes water and energy, and we treat both as costs to be controlled and impacts to be reduced. Our sites run closed-loop water treatment: process water from wipe production is treated and returned to non-contact use, and exhaust air is filtered before discharge. The EDI purified water system that feeds our lines is designed to minimise reject water, and because a large part of our disinfection chemistry is based on electrolysed water, chemical discharge stays low.
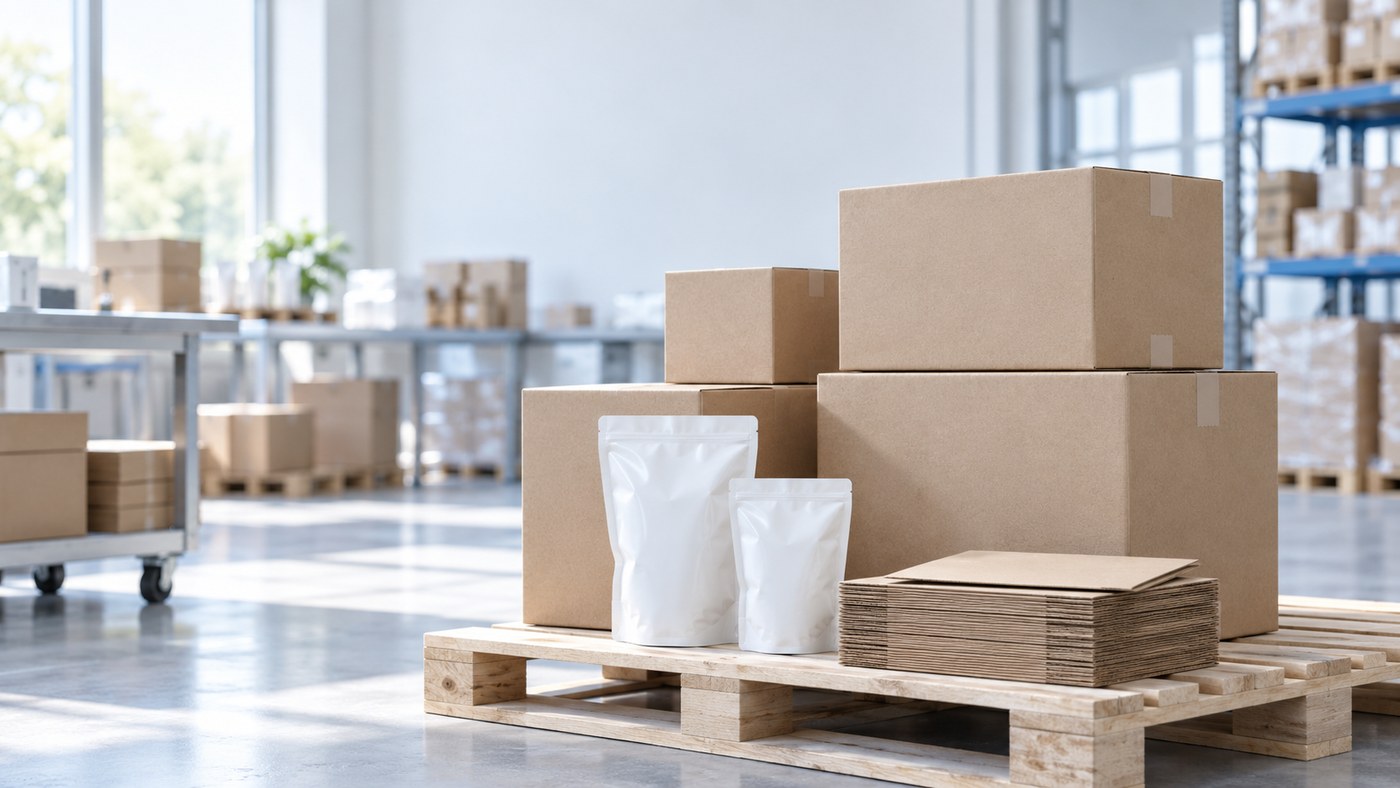
FSC-certified cardboard and reduced-plastic packaging used by GemmyMedical
Greener packaging materials
Packaging is the most visible part of a product's environmental footprint. We build with FSC-certified fibre and cardboard for cartons and canisters, keep plastic content per unit as low as shelf life allows, and supply biodegradable sample bags for distributor sampling. For OEM and private-label projects we design reduced-packaging options in at specification stage: refill pouches, bulk formats and cartons with recycled content.
Send a message
If you have any questions about our products or others, please leave a message.
ver_code
CONTACT
John Ouyang
John Ouyang
John Ouyang
COO and VP Marketing
Tel: +86 18317128098
WeChat: +86 18317128098
Whatsapp: +86 18317128098
Justin Khaydarov
Justin Khaydarov
Justin Khaydarov
Sales manager
Tel: +86 18621998738
WeChat: +86 18621998738
Whatsapp: +86 18621998738
Roy Liu
Roy Liu
Roy Liu
Sales manager
Tel: +86 17673208570
WeChat: +86 17673208570
Whatsapp: +86 17328019718
Max Ylham
Max Ylham
Max Ylham
Sales manager
Tel: +86 13033481775
WeChat: +86 13033481775
Whatsapp: +86 13033481775